Hinada Delivers 80 m³/day Containerized MBR System to Pakistan Client
Hinada has completed the delivery of a containerized MBR wastewater treatment system to a client in Pakistan, with a design capacity of 80 m³/day. The project demonstrates how compact, prefabricated membrane bioreactor technology can meet decentralized sewage treatment needs in regions where civil construction is slow, land is limited, and reliable operation matters more than elaborate plant infrastructure.
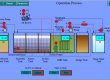
The system integrates equalization, biological treatment, membrane separation, and disinfection within a standard container footprint. At its core are Hinada’s PVDF hollow-fiber MBR membrane modules, which retain biomass and suspended solids while producing clear permeate suitable for discharge or reuse. The containerized configuration allows the entire unit to be fabricated and pre-tested at the factory, shipped as a single package, and commissioned on site with minimal piping and civil works—an advantage for overseas projects where site conditions and construction schedules are difficult to control.
For the Pakistan client, the 80 m³/day capacity matches a community or facility-scale demand: large enough to handle real sewage flows, small enough to remain manageable for local operators. The system is designed for straightforward operation, with online monitoring and membrane integrity testing supporting stable performance and predictable maintenance.
A new operation video walks through the delivery and setup: the container being prepared for shipment, the membrane modules and blower/control skid in place, and the system running in containerized operation. It shows what “plug-and-play” means in practice—not a slogan, but a factory-built treatment plant that arrives ready to connect, start up, and produce consistent effluent. For clients comparing options for rural, remote, or fast-track wastewater projects, the video offers a concrete look at how Hinada’s containerized MBR System approach turns into a reliable, operable MBR system.